Recent innovations in large capacity refrigerated centrifuge wholesale technology focus on the improvement of automation as well as information integration. Intelligent models now communicate with laboratory information management systems so that the recording of experimental parameters is no longer problematic. Noise reduction modules and ergonomic covers have also increased user comfort and safety. Also, controlled temperature chambers and high-speed rotors facilitate the handling of sensitive material without degradation. Such technology renders large capacity refrigerated centrifuge wholesale equipment more adaptable to varying research needs, offering unparalled precision in particle separation and purification processes in countless industries.
The versatility of large capacity refrigerated centrifuge wholesale can be seen in its application to numerous specialized fields. In marine biology, it helps one analyze plankton and microbial samples. In food science, it helps with the accurate measurement of fat and protein content. The electronics sector employs large capacity refrigerated centrifuge wholesale for purifying liquid crystals and conductive materials. In environmental protection, large capacity refrigerated centrifuge wholesale facilitate tracking of pollutants and studies on recycling. They aid in veterinary medicine in blood diagnosis and disease investigation. With these uses, large capacity refrigerated centrifuge wholesale bring about innovation through offering dependable means for analyzing as well as separating materials.
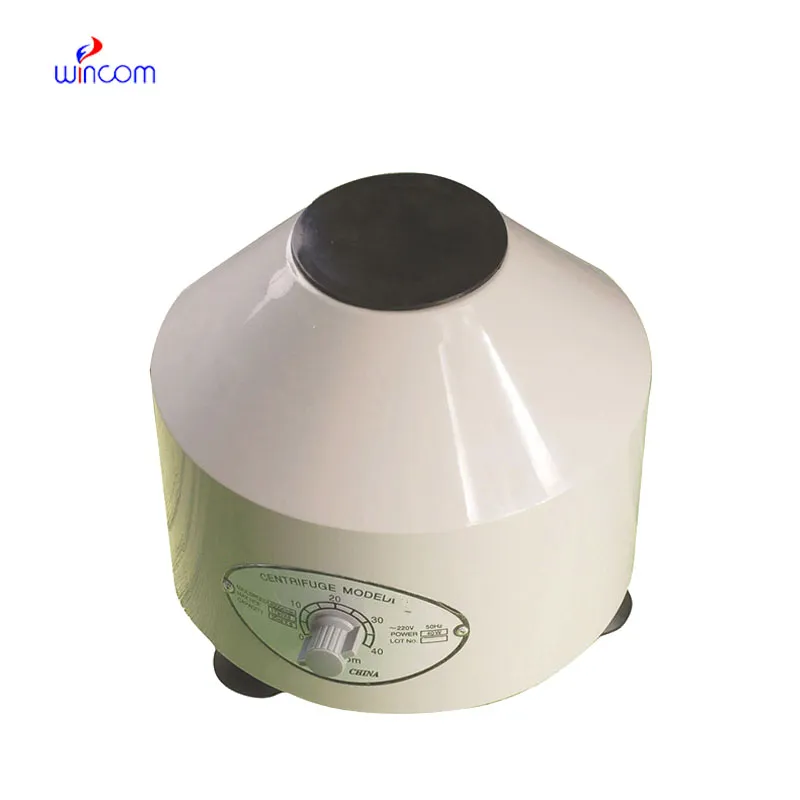
{Keywords} of the future will unprecedentedly advance in performance and design. Future systems will feature adaptive balancing technology that adjusts to dynamic loads in real time. Intelligent rotors will track stress and fatigue in real time, allowing for extended service life. With IoT connectivity, multiple large capacity refrigerated centrifuge wholesale units will be remotely managed to streamline laboratory networks. In biomedical applications, miniaturized devices will facilitate high-throughput screening with low sample volumes. These advancements are a step toward smarter, faster, and greener devices that revolutionize how separation processes are controlled in modern science.
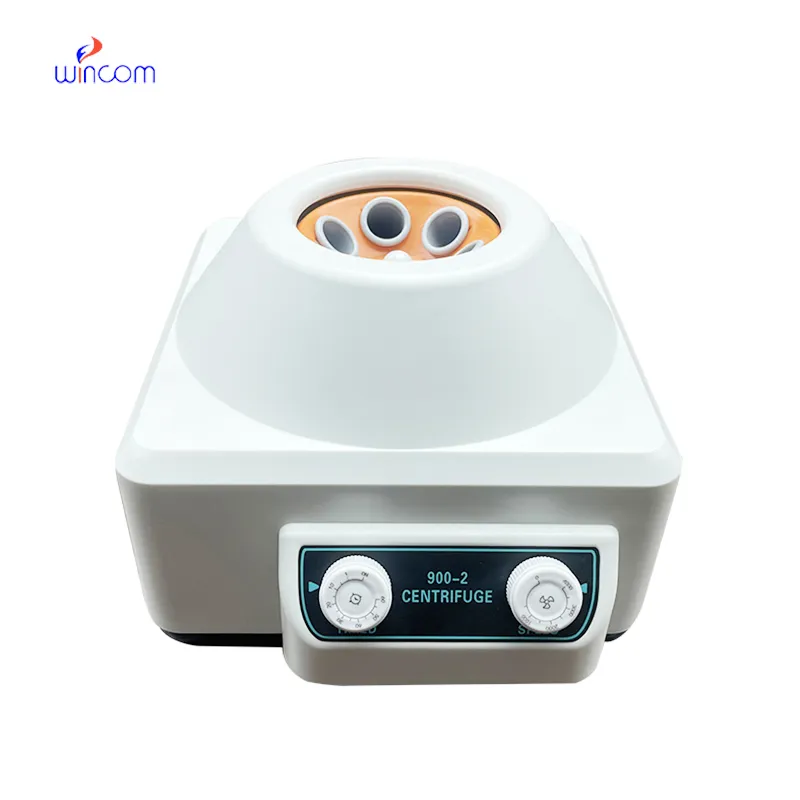
Maintenance of large capacity refrigerated centrifuge wholesale is essential to lab safety and data integrity. Cleaning should be performed immediately following every operation, with special attention to the elimination of any liquid spills or residues from samples. The rotor should always be handled gently, placed in an upright position during storage, and never subjected to shock. Periodic inspection of lid locks and gaskets ensures airtight operation. Power cord and fuse conditions should also be checked by operators. Annual servicing by skilled technicians adds lifespan. Through regular care processes, large capacity refrigerated centrifuge wholesale safely and accurately continues to operate.
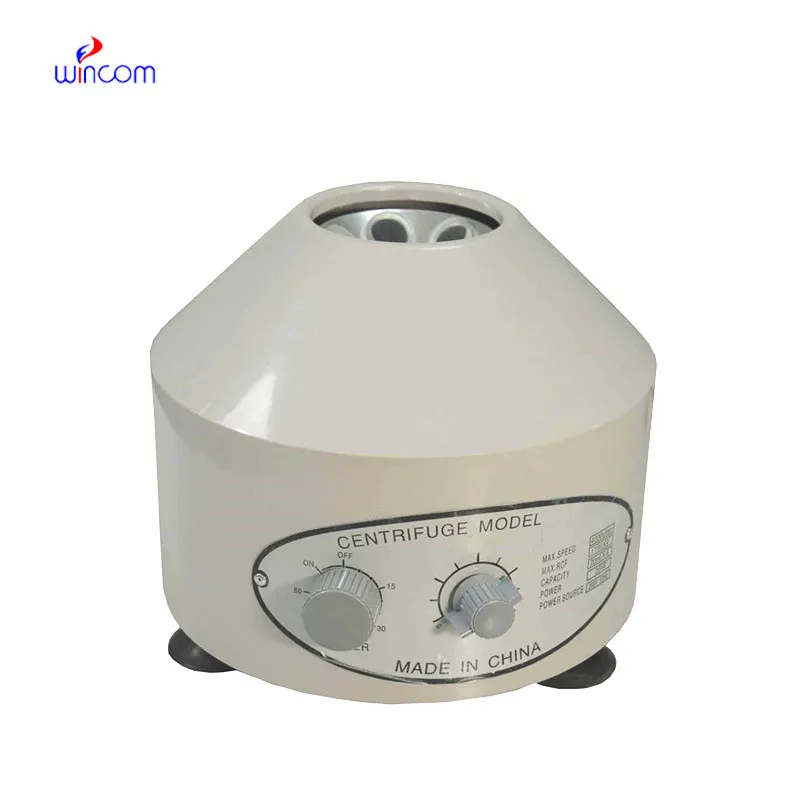
A large capacity refrigerated centrifuge wholesale operates by inducing centrifugal force through rapid rotation, separating substances according to mass and density. It has a critical use in laboratories, medical testing, and industrial treatment. In medicine, for instance, large capacity refrigerated centrifuge wholesale facilitate plasma and serum separation for the purpose of diagnosis. In environmental science, they assist in the examination of suspended solids in water samples. Their robust build, combined with programmable functions and safeguarding features, facilitates fine speed control and timing. large capacity refrigerated centrifuge wholesale continue to evolve to provide faster and more accurate separation procedures in various fields.
Q: How is a centrifuge different from a mixer or shaker? A: Unlike mixers or shakers that blend materials, a centrifuge separates components based on density through high-speed rotation. Q: What power requirements does a centrifuge need? A: Most benchtop centrifuges use standard AC power, while industrial units may require higher voltage for greater speed and capacity. Q: Can a centrifuge be used in pharmaceutical production? A: Yes, centrifuge equipment is widely used to purify chemical compounds and biological materials during drug manufacturing processes. Q: How do I prevent vibration during operation? A: Ensure all tubes are evenly loaded, rotors are clean, and the machine is placed on a stable, level surface. Q: What is the lifespan of a centrifuge? A: With regular maintenance and proper usage, a centrifuge can last for many years while maintaining consistent performance.
We’ve been using this mri machine for several months, and the image clarity is excellent. It’s reliable and easy for our team to operate.
The delivery bed is well-designed and reliable. Our staff finds it simple to operate, and patients feel comfortable using it.
To protect the privacy of our buyers, only public service email domains like Gmail, Yahoo, and MSN will be displayed. Additionally, only a limited portion of the inquiry content will be shown.
We are planning to upgrade our imaging department and would like more information on your mri machin...
I’m looking to purchase several microscopes for a research lab. Please let me know the price list ...
E-mail: [email protected]
Tel: +86-731-84176622
+86-731-84136655
Address: Rm.1507,Xinsancheng Plaza. No.58, Renmin Road(E),Changsha,Hunan,China
 EN
 af
 es
 ar
 tr
 sw
 pt
 th
 ur
 bn
 ne
 vi
 km
 lo
 de
 ru
 fi
 nl
 fa
 fr
 ko