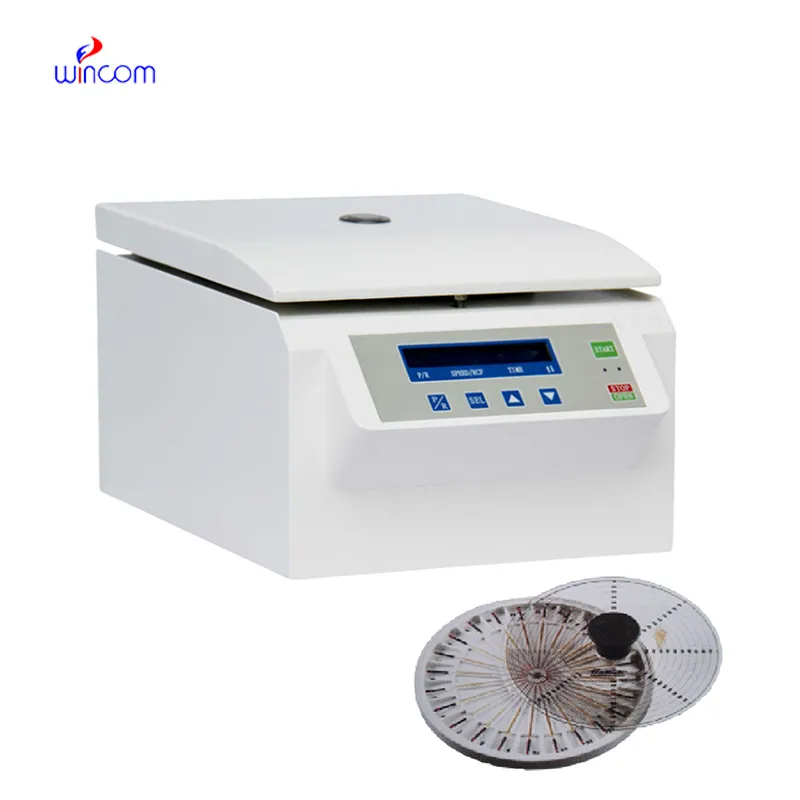
The operation of an super large capacity refrigerated centrifuge largely relies on its rotor design, accuracy in balancing, and operating speed. Modern models typically come with programmable interfaces that allow users to control acceleration rates, temperature, and run times with great accuracy. Some advanced super large capacity refrigerated centrifuge incorporate vibration sensing and auto-imbalances for stabilizing high-speed rotation. Additionally, the use of light but strong materials like carbon fiber enhances safety and energy efficiency. This marriage of engineering ingenuity and electronic control combines the super large capacity refrigerated centrifuge into a reliable partner for research and production environments.
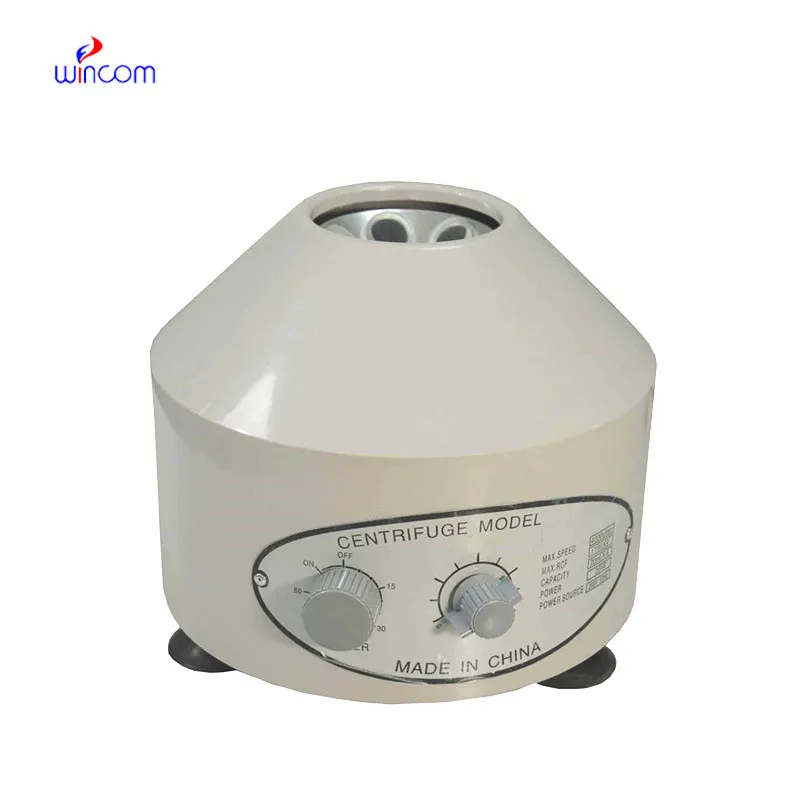
The utilitarian uses of super large capacity refrigerated centrifuge have expanded due to technological advancements. It is utilized in pharmacology to ensure high-purity drug formulations. It is utilized in biotechnology for protein crystallization and vaccine synthesis. The extractive industry utilizes super large capacity refrigerated centrifuge to separate valuable minerals from raw mixture. In classrooms, it facilitates laboratory demonstrations of fluid flow. Even in the restoration of paintings, expert super large capacity refrigerated centrifuge facilitate cleaning and stabilizing delicate pigments. The applicability of super large capacity refrigerated centrifuge to so many different fields is evidence of its utility as an industrial and scientific agent for material separation.
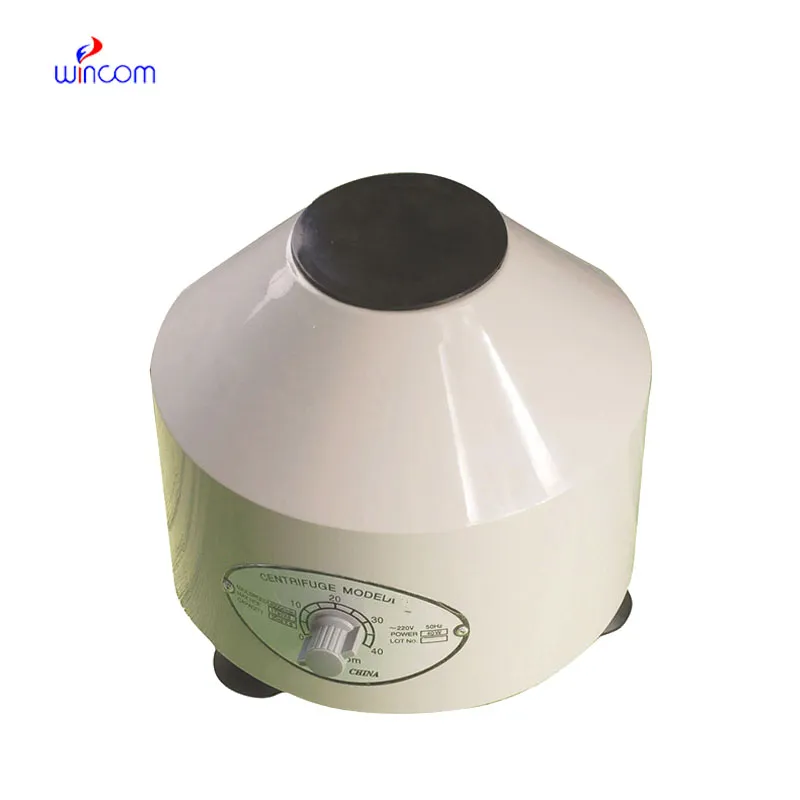
The super large capacity refrigerated centrifuge of the future will be innovative, intelligent, and integrated. With the advent of smart manufacturing, super large capacity refrigerated centrifuge systems will operate independently on predictive analytics. Programs with machine learning will interpret vibration patterns to optimize performance with minimal human involvement. Renewable energy integration will make operation more sustainable, and modular design will facilitate instant replacement of parts. Data visualization software will be more sophisticated, providing real-time feedback on the separation process. This blend of mechanical precision and intelligent technology will place super large capacity refrigerated centrifuge at the forefront of international scientific advancement.
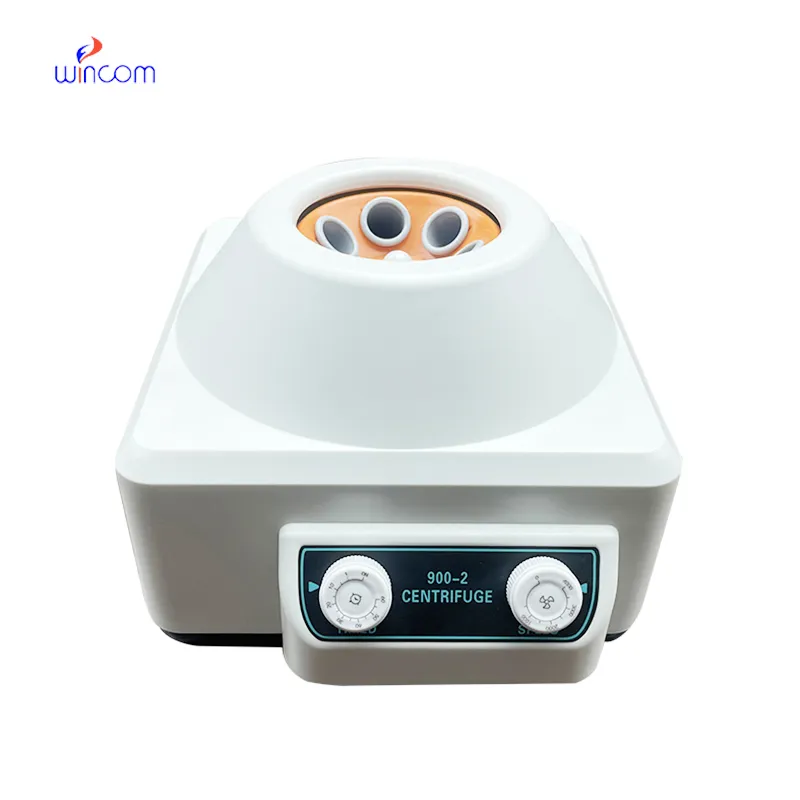
Maintenance of super large capacity refrigerated centrifuge is essential to lab safety and data integrity. Cleaning should be performed immediately following every operation, with special attention to the elimination of any liquid spills or residues from samples. The rotor should always be handled gently, placed in an upright position during storage, and never subjected to shock. Periodic inspection of lid locks and gaskets ensures airtight operation. Power cord and fuse conditions should also be checked by operators. Annual servicing by skilled technicians adds lifespan. Through regular care processes, super large capacity refrigerated centrifuge safely and accurately continues to operate.
Through controlled rotation, a super large capacity refrigerated centrifuge produces very high outward pressure that separates the components of a mixture. It is used comprehensively in medical diagnosis, chemical analysis, and materials science. Its efficacy lies in uniform velocity and balance, producing neat separation of liquids and solids. Most super large capacity refrigerated centrifuge today have digital timers, automatic lid closing, and temperature regulation. Such the inclusion of safety and efficiency has made the super large capacity refrigerated centrifuge a staple of modern research and manufacturing, providing faster and more accurate results across industries.
Q: What is a centrifuge used for? A: A centrifuge is used to separate mixtures based on density differences by spinning them at high speeds, allowing heavier particles to settle away from lighter ones. Q: How does a centrifuge work? A: A centrifuge operates by generating centrifugal force, pushing denser materials outward while lighter components remain near the center, resulting in effective separation. Q: What are common applications of a centrifuge? A: Centrifuges are used in laboratories, hospitals, and industries for blood testing, chemical analysis, purification, and sample preparation. Q: How often should a centrifuge be calibrated? A: Calibration should be performed at least once a year or whenever performance inconsistencies appear to ensure accuracy and reliability. Q: Can a centrifuge handle biological samples? A: Yes, many centrifuges are designed for biological materials such as blood, plasma, and cell cultures under controlled and sterile conditions.
This ultrasound scanner has truly improved our workflow. The image resolution and portability make it a great addition to our clinic.
I’ve used several microscopes before, but this one stands out for its sturdy design and smooth magnification control.
To protect the privacy of our buyers, only public service email domains like Gmail, Yahoo, and MSN will be displayed. Additionally, only a limited portion of the inquiry content will be shown.
I’d like to inquire about your x-ray machine models. Could you provide the technical datasheet, wa...
Hello, I’m interested in your water bath for laboratory applications. Can you confirm the temperat...
E-mail: [email protected]
Tel: +86-731-84176622
+86-731-84136655
Address: Rm.1507,Xinsancheng Plaza. No.58, Renmin Road(E),Changsha,Hunan,China
 EN
 af
 es
 ar
 tr
 sw
 pt
 th
 ur
 bn
 ne
 vi
 km
 lo
 de
 ru
 fi
 nl
 fa
 fr
 ko